
High-Performance Modular Cleanroom Solutions
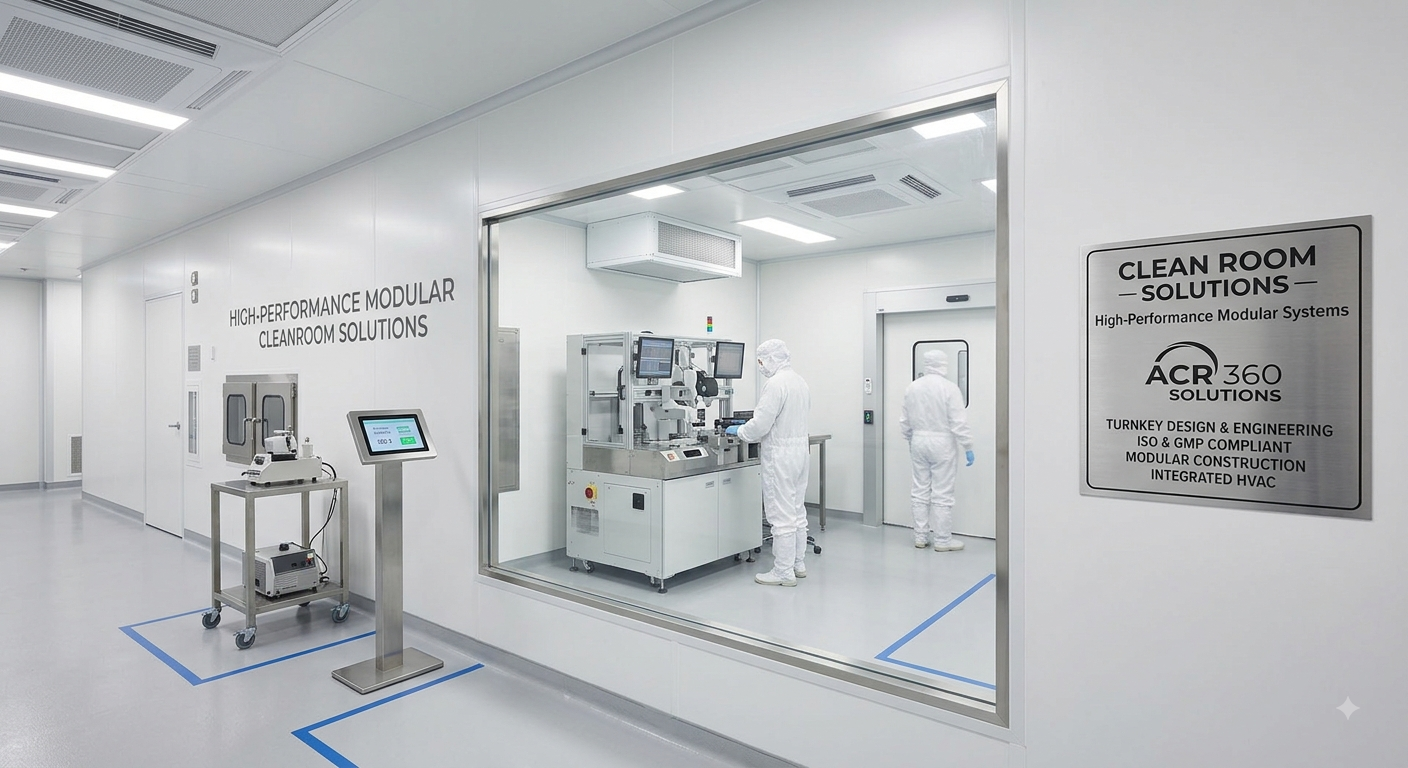
Tagline / Subheading: Turnkey Design, Engineering, and Installation for Contamination-Controlled Environments
Overview We design, manufacture, and install custom, high-precision cleanroom environments tailored to strict industry compliance standards. From modular wall systems and HVAC filtration to complete turnkey facilities, our engineering ensures maximum particle control, air purity, and operational efficiency.
Key Features & Capabilities:
- Turnkey Manufacturing: Full end-to-end execution, from initial CAD layout and panel fabrication to site assembly and validation.
- ISO & GMP Compliance: Built to meet ISO Class 1 through Class 8 standards, as well as EU GMP and FDA requirements.
- Modular Wall & Ceiling Panels: Durable, flush-surface panels engineered for easy sterilization, thermal insulation, and minimal particle retention.
- Integrated HVAC & Air Filtration: Heavy-duty air handling units equipped with HEPA/ULPA filtration to maintain precise pressure differentials, temperature, and humidity.
- Custom Doors & Accessories: Air showers, pass-through boxes, cleanroom doors, and interlocking systems designed to prevent cross-contamination.
Industries Served :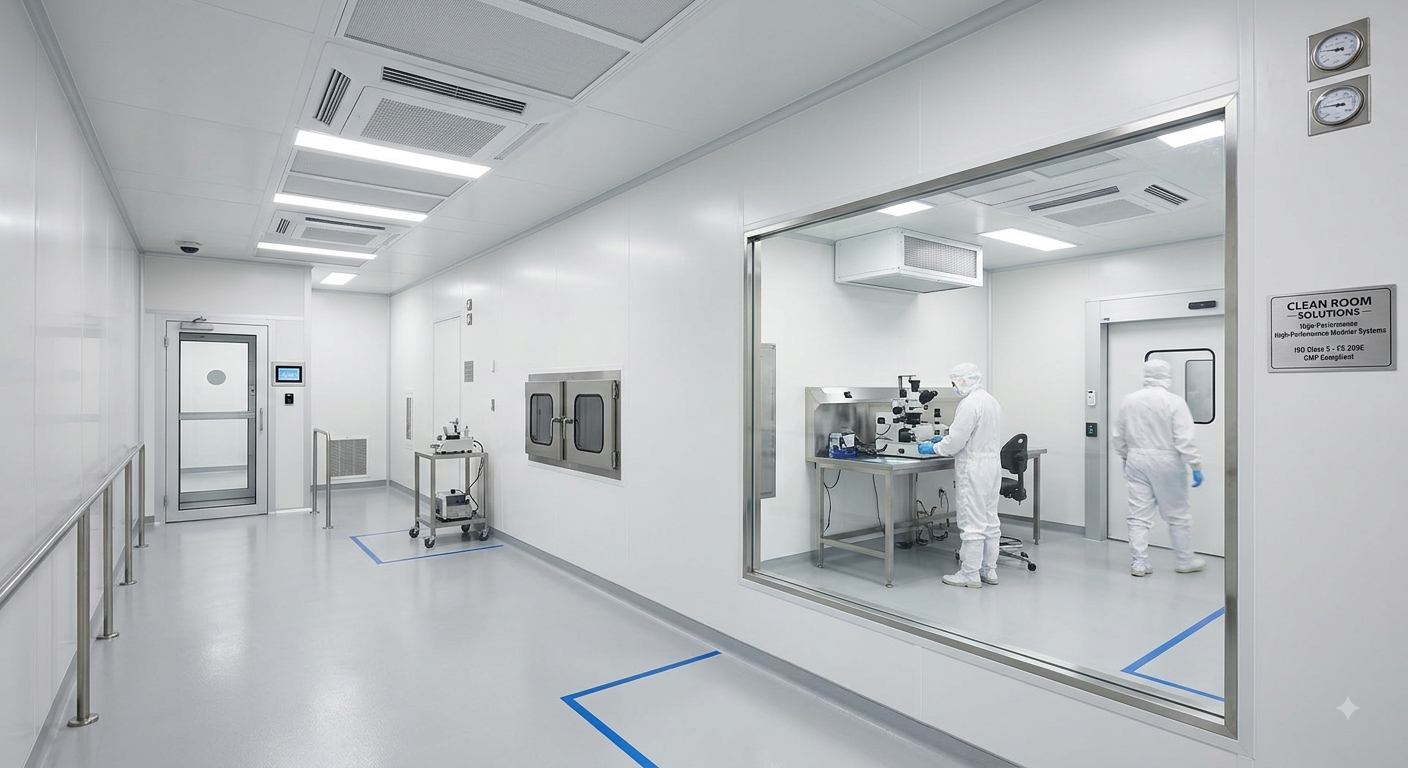
- Pharmaceuticals & Biotechnology: Sterile compounding, drug packaging, and active pharmaceutical ingredient (API) processing.
- Semiconductor & Electronics: Precision microchip assembly, optics, and nanofabrication.
- Medical Devices: Sterile packaging, implant manufacturing, and diagnostic assembly.
- Research Laboratories & Healthcare: Isolation rooms, gene therapy labs, and specialized hospital environments.
Why Partner With Us:
- Custom Engineering: Tailored layout design based on your process airflow and spatial constraints.
- Rapid On-Site Installation: Modular components allow faster assembly times with minimal facility downtime.
- Rigorous Testing & Validation: Full support for commissioning, particle counting, and compliance documentation.